
Liquid level sensors are used for real-time detection of liquid level height. They convert liquid level signals into standard electrical signal outputs, serving as core sensing components in automated processes. They have been widely deployed in industrial automation, textile, water treatment, food and beverage, and many other fields, playing a vital role in various fluid control scenarios.
Lanbao Ultrasonic Level Sensors | Fully Adaptable, Easily Controlled
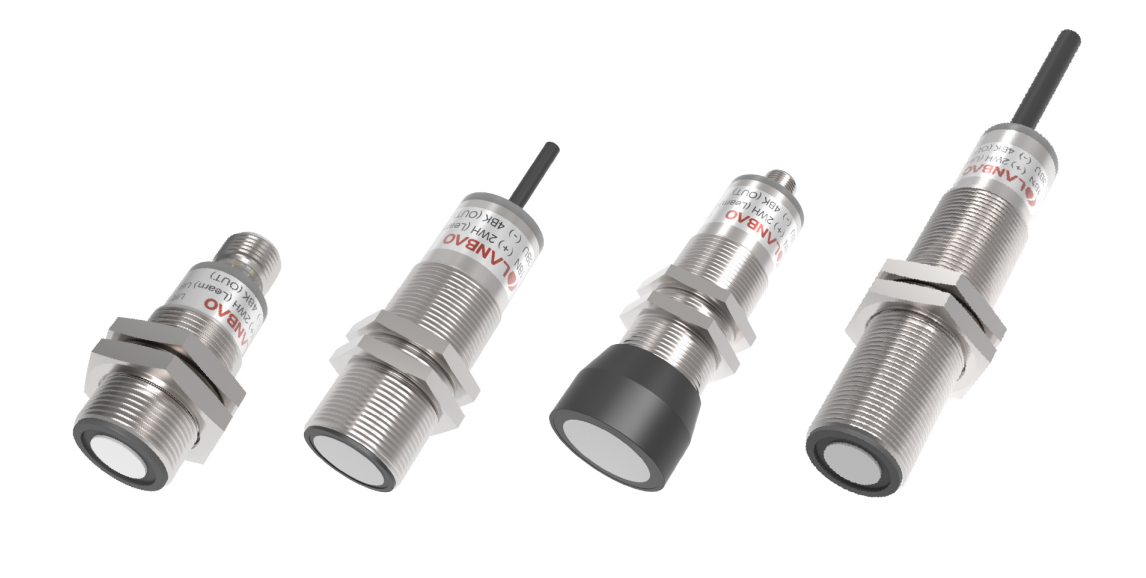
• Unaffected by liquid color, it delivers stable detection of liquid and object height.
• Available in multiple outer diameter sizes including M12, M18 and M30, for easy adaptation to the mounting structure and space requirements of different equipment.
• Detection range from 15 cm to 6 m. The wide measuring range suits most industrial automation detection applications.
• IP67 protection rating: dustproof, moisture-proof and stain-resistant. It can operate stably for a long time outdoors and in harsh environments with dust and high humidity.
• Equipped with a teach-in wire for fast detection distance configuration, enabling flexible and convenient on-site commissioning.
• Supports multiple output types including digital switching, analog and RS485 communication, for simple connection to PLC and host systems.
Lanbao Capacitive Level Sensors | Precision & Stability, Preferred Cost-effective Solution
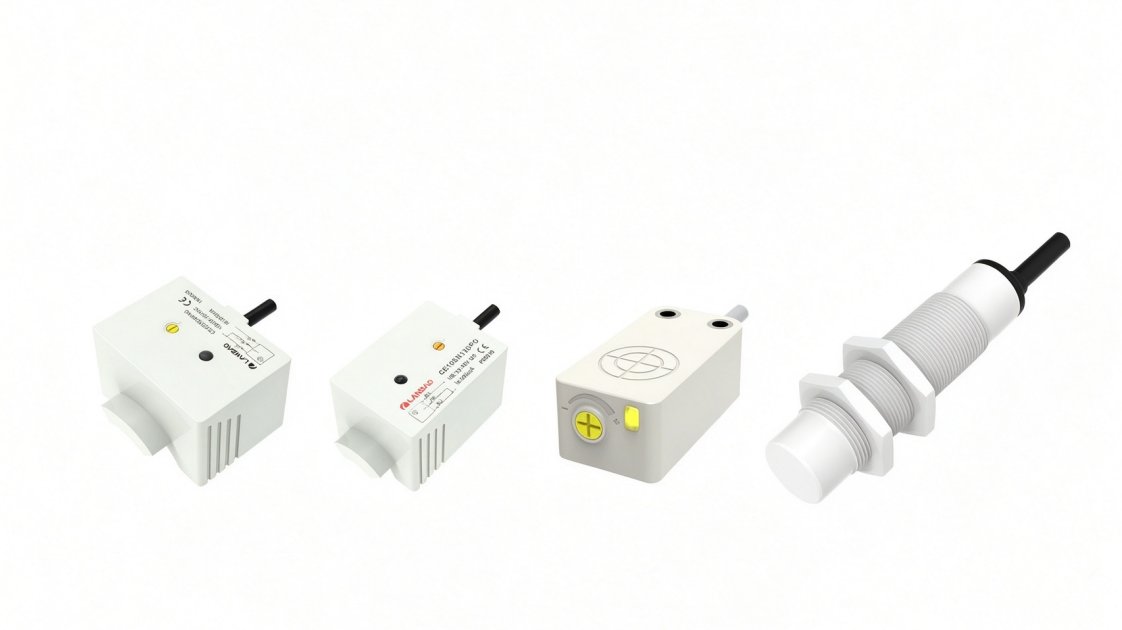
• Compact housing, ideal for space-limited applications. Widely used in dispensing equipment and small liquid level control systems.
• It detects liquid level status by sensing capacitance variation of the medium, delivering accurate measurement to ensure stable liquid level control.
• Compliant with IEC60947-5-2 test standard. It maintains reliable signal output even under working conditions with strong electromagnetic interference.
• The sensing distance is adjustable via a multi-turn potentiometer, with a maximum sensing distance of 8 mm.
• The sensor does not come into direct contact with the measured medium, eliminating risks of material contamination and probe corrosion. • Outstanding cost performance, suitable for mass deployment on production lines.
In-depth Application Across Multiple Industries, Empowering Automated Fluid Control
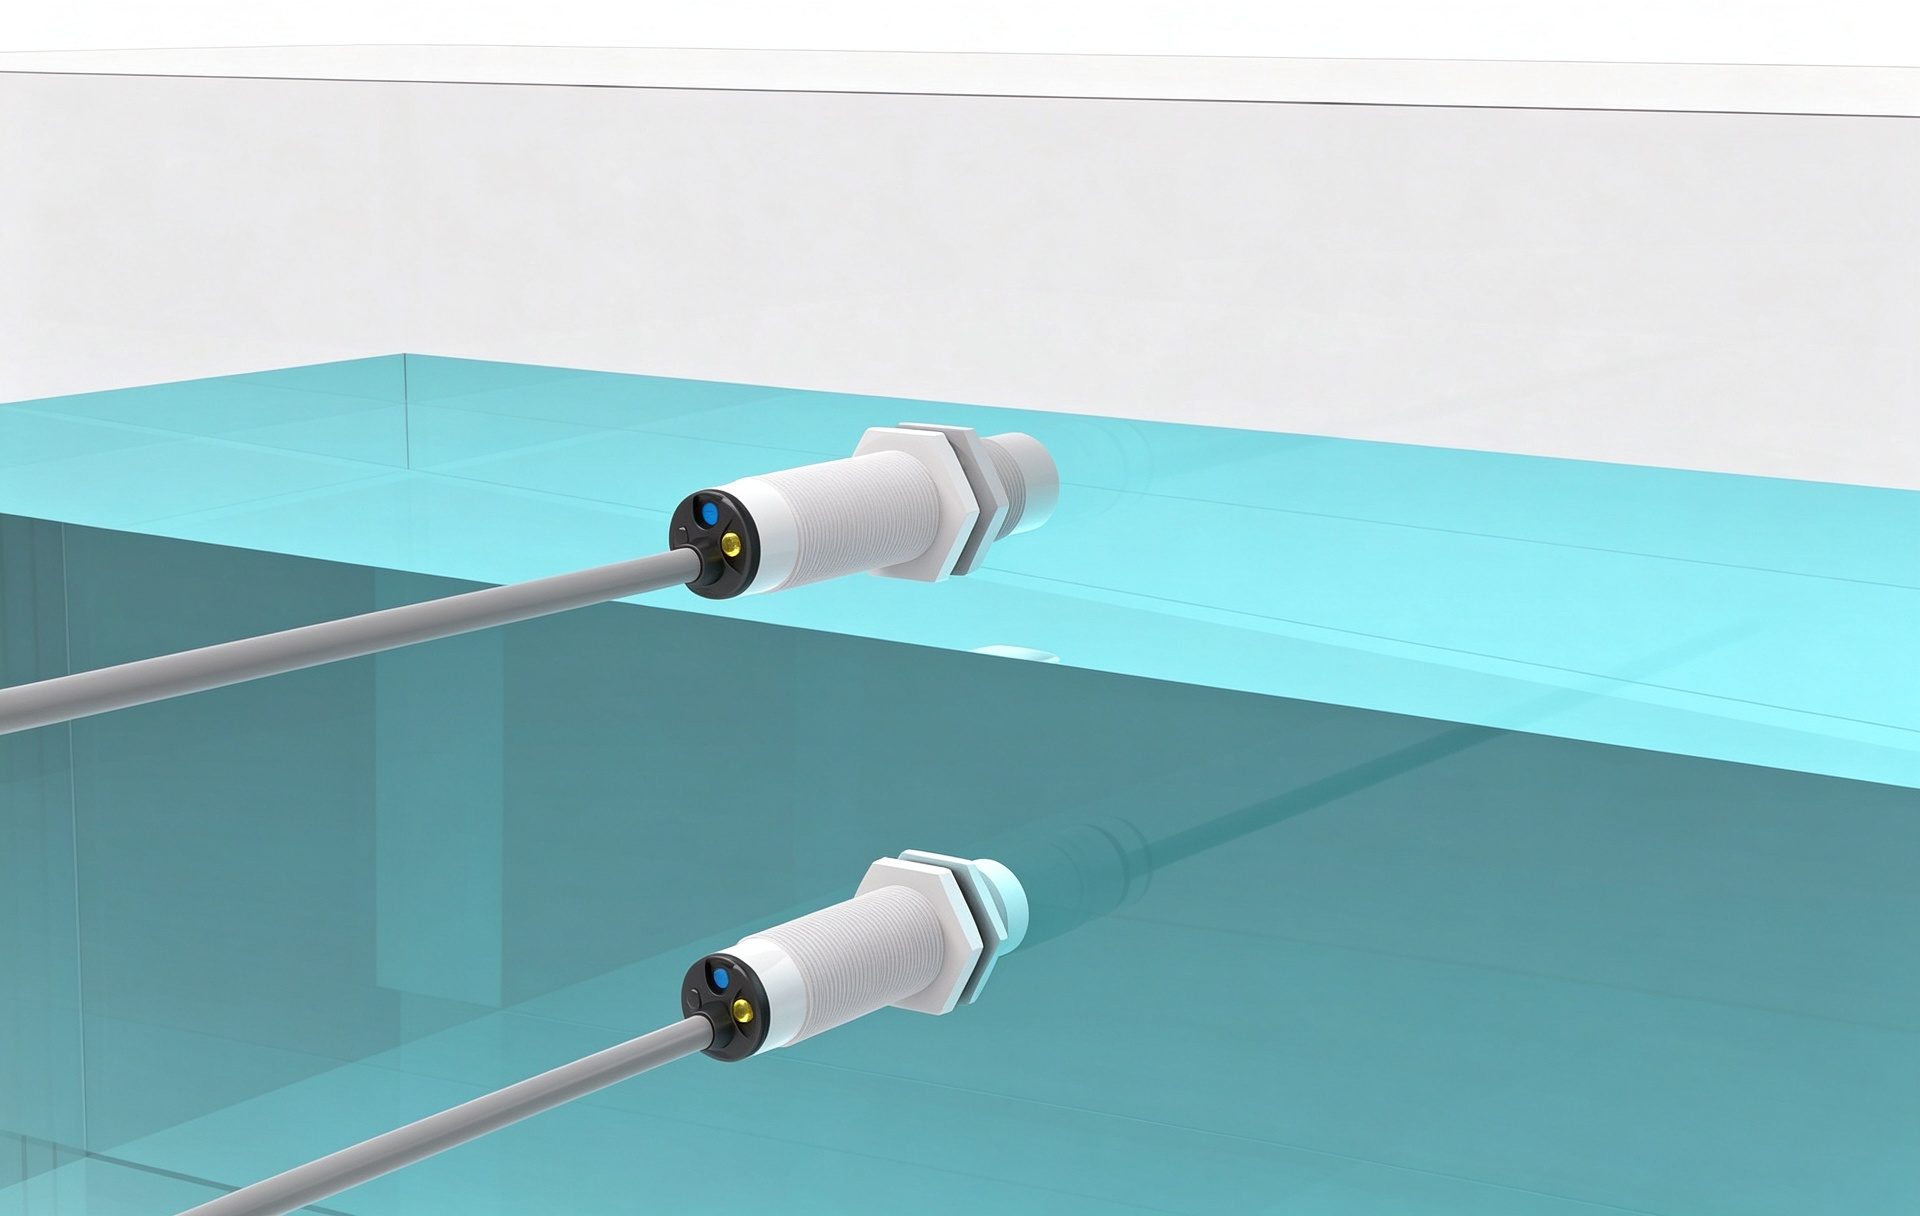
Real-time Liquid Level Monitoring
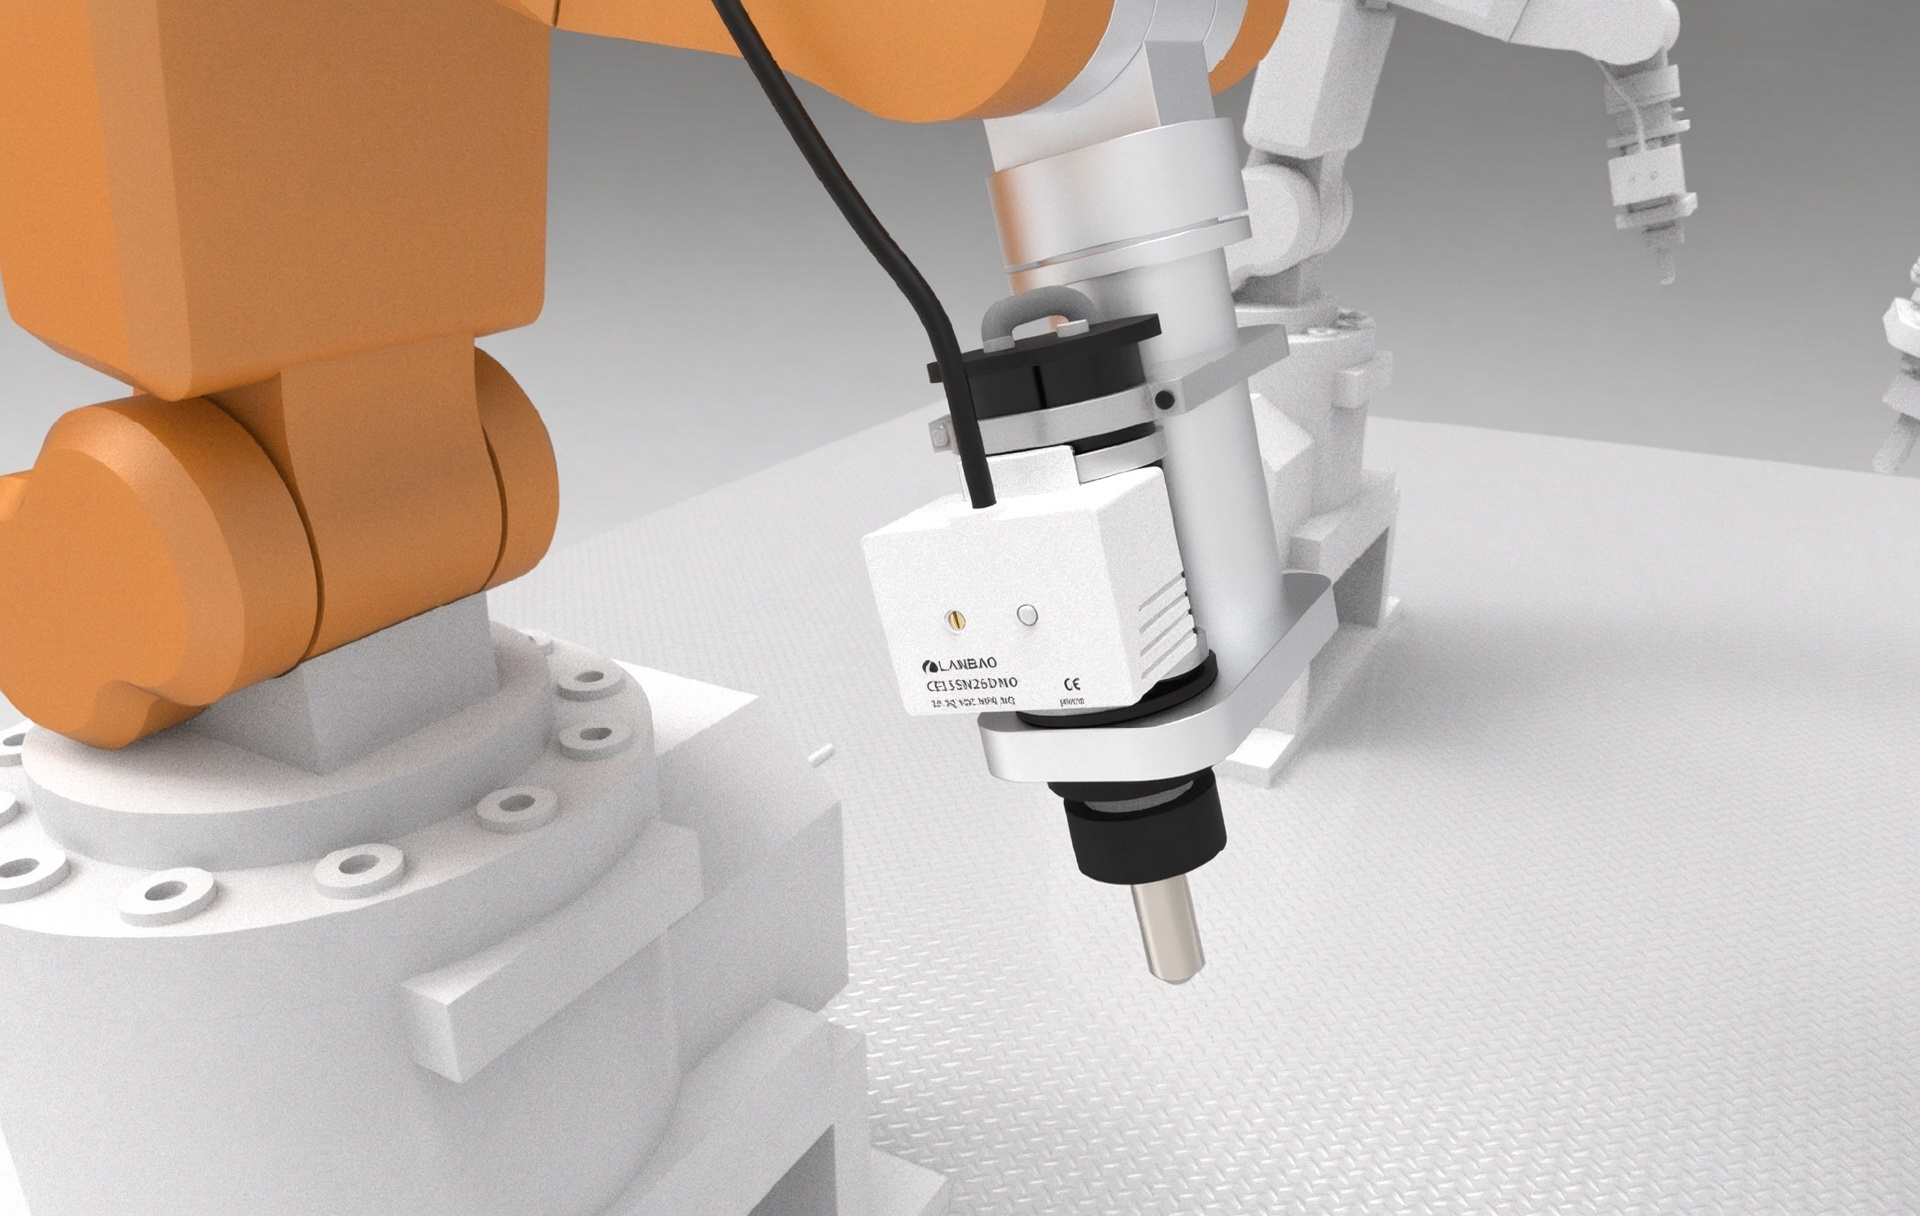
Glue Residue Detection for Dispensing Equipment
Constant Buoyancy Level Detection
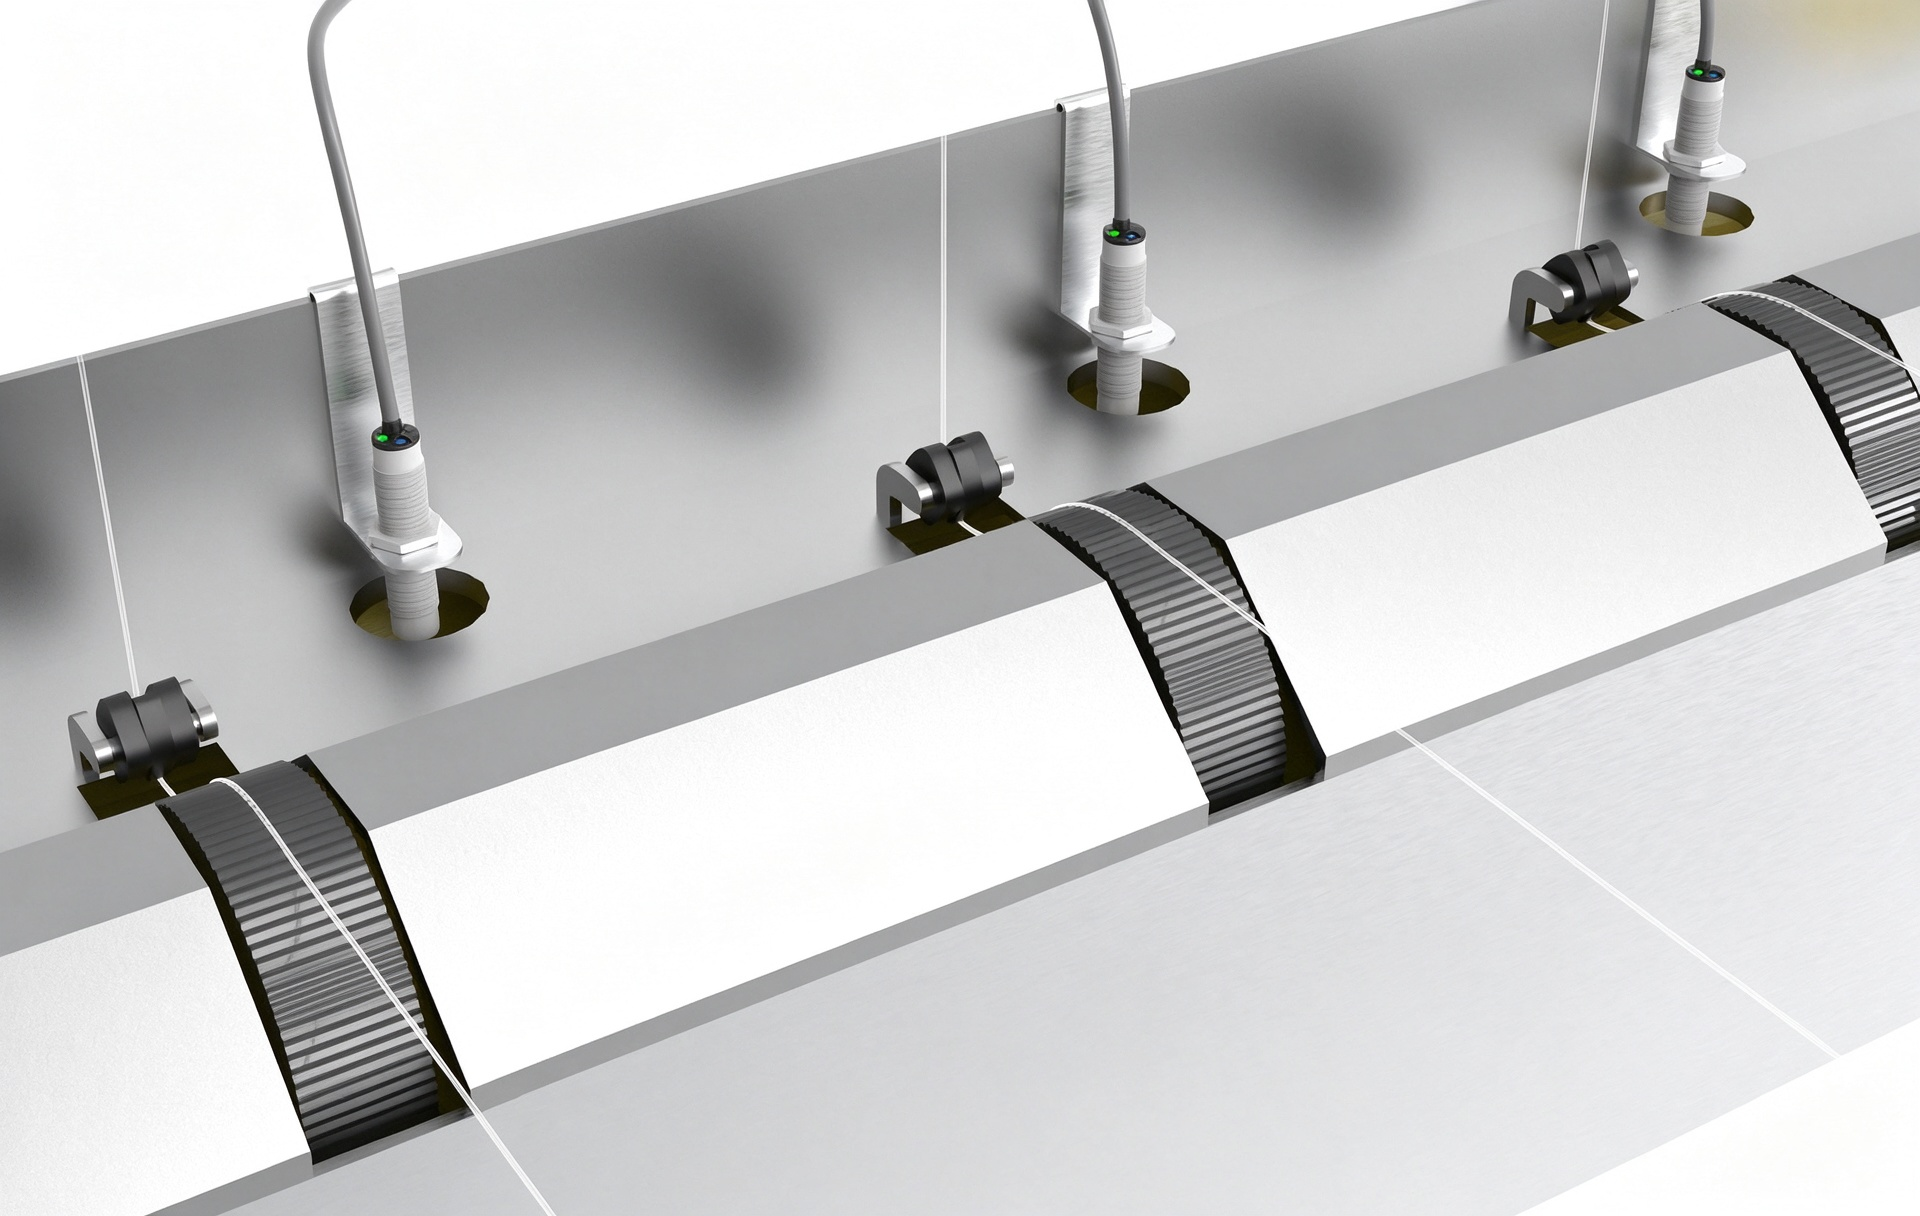
With a comprehensive portfolio of liquid level detection solutions, Lanbao Sensing covers diverse monitoring scenarios including storage tanks, pipelines and various special-purpose equipment, capturing liquid level variation signals with high precision. Its stable and reliable sensing capability provides solid data support for automated closed-loop control, helping fluid processes operate efficiently and safely.
Post time: Nov-09-2026